Kalup - Supplier Quality Portal for SCARs, 8D Reviews and Scorecards
Supplier Quality Platform for a Serbian Machinery Maker
Designed and built a clickable supplier quality console for a Serbian maker of tractors, telehandlers and backhoe loaders: raise supplier corrective action requests, drive containment and 8D problem solving to a verified root cause, track the cost of each defect and score about 450 suppliers on a published formula.
Most of our work is under NDA. Per agreement, we can share the work but not the company details - all names and identifying information shown here have been changed.
Impact
Dashboard, SCAR list in table and board views, SCAR detail with 7 tabs, the 8D review workspace and supplier scorecards. Every one of the 26 demo SCARs opens its own detail page.
Each 8D step has its own review checklist, 22 checks in all. Root cause covers both why the defect was made and why it escaped, each with 5 Whys and a 6-branch fishbone.
Due dates are set from the client's response targets when a SCAR is raised: containment in 24 hours, root cause in 10 working days, corrective action in 30 days. Safety SCARs get 8 hours and 5 working days.
24 suppliers in 10 countries, 24 parts with their key drawing characteristic, 21 defect codes in English and Serbian, 3 plants, 7 staff users and 5 supplier escalations.
The Problem
Fruškadol ran supplier quality on email, a shared drive of Excel 8D templates and a spreadsheet of open complaints per plant. The same defective casting could be reported to the same foundry by two plants a week apart, suppliers sent 8D reports as PDFs weeks late with "operator error" as the root cause, nobody checked whether fixes worked, sort and line stoppage costs were rarely charged back, and the quarterly supplier scorecard took one engineer four days to build by hand.
Our Solution
Kalup gives Fruškadol's supplier quality engineers one console for every non-conformance across 3 plants: raise a SCAR against the supplier, follow containment and each 8D discipline to its due date, accept or return each step against a checklist, collect the costs as evidence for recovery, and score suppliers on a fixed formula before publishing the results to them.
The Challenge: Quality Across Two Companies
Fruškadol builds farm and construction machinery in 3 assembly plants and buys direct material from about 450 suppliers in Serbia, the wider region and the EU. Supplier quality follows ISO 9001 and, as client policy, IATF 16949-style practice: 8D problem solving, PPAP, controlled shipping and scorecards. Every defect involves people on both sides of the contract.
The Same Defect, Reported Twice
A cracked axle housing casting found at Rumenka could be reported to the same foundry by another engineer at Temerin a week later, with neither knowing. Without one record per supplier, part and defect code, repeat problems looked like new ones.
Root Causes Nobody Checked
8D reports arrived as PDFs, often late, and "operator error" was accepted with nothing behind it. Containment has to be in place before root cause work counts, the cause has to explain why the defect also escaped, and a fix is not closed until later deliveries prove it worked.
Costs Without Evidence
The supplier quality agreement lets Fruškadol recover sorting, rework, scrap, line stoppage and admin costs at published rates, but nobody could assemble the sort records, scrap tickets and stoppage minutes behind a claim, so most costs were never charged back.
Scorecards Built by Hand
One engineer spent four days each quarter building the supplier scorecard from spreadsheets. Escalation to formal warning or controlled shipping depended on numbers nobody could easily rebuild, and suppliers could not see how their own score was worked out.
Our Approach: From 8D Practice to a Clickable Console
Spec and Rules Research
Mapped 11 user roles across the quality console and the supplier portal, 42 screens (33 console, 9 portal) and the data model for suppliers, parts and drawing characteristics, receipts, SCARs, 8D disciplines, evidence, sort results, cost lines, chargebacks, PPAP, first article inspections, audits, escalations and controlled documents. Wrote down the rules the design follows: 8D discipline order, the response targets, rate card and approval limit, the scorecard formula and escalation levels, AIAG PPAP elements and levels, Serbia's Law on Personal Data Protection for supplier contacts, and the EU Machinery Regulation for machines sold into the EU.
Clickable Demo on a Production UI Kit
Built the quality console's 5 key screens on a production dashboard kit: the dashboard with supplier ppm against target, open and overdue SCARs, SCARs by stage and a My work list that changes with the demo role; the SCAR list with filters, bulk actions and a quick view panel; SCAR detail with the D1 to D8 progress rail, containment, evidence, costs, messages and activity; the 8D review workspace; and scorecards with a publish step. Accepting or returning a discipline, recording sort results, confirming containment and adding costs update counts and stages across screens on local state.
What a Production Build Adds
Integration with the ERP (such as SAP S/4HANA or Dynamics 365) for goods receipts, inspection lots, quality holds and debit notes through Serbia's SEF e-invoicing, the PLM for drawings, and the plant MES for line failures. Staff single sign-on, supplier sign-in with MFA, evidence stored in an EU region, an append-only audit log, and the remaining screens: New SCAR on a tablet, the containment board, verification queue, chargebacks, PPAP and FAI, audits, escalations, document control, reports, settings and the 9-screen supplier portal.
Why It Works: Every Fix Has to Be Proven
Root Cause Must Explain the Escape
The D4 review splits why it was made from why it was not detected, each with numbered 5 Whys and a fishbone whose causes are marked ruled out, possible or confirmed with their evidence. A step is accepted only when every check on its list is ticked, and "operator error" alone is not accepted.
Repeats Show Up Across Plants
A SCAR with the same supplier, part and defect code within 180 days carries a repeat badge and links to the earlier ones, so a defect found at Temerin points straight to the Rumenka SCAR from the same heat number.
Due Dates Come From Policy
Each discipline's due date is fixed from the response targets the moment a SCAR is raised, with tighter targets for safety-relevant parts. Stages holding overdue SCARs turn amber on the dashboard, and steps waiting on Fruškadol's own review never count against the supplier.
A Scorecard Suppliers Can Check
Scores combine quality from ppm against the commodity target, on-time in-full delivery and 8D steps submitted on time, weighted 50, 30 and 20 percent, with a worked example on screen. A period stays a draft until it is published, which locks the scores.
Related case studies
View all: Manufacturing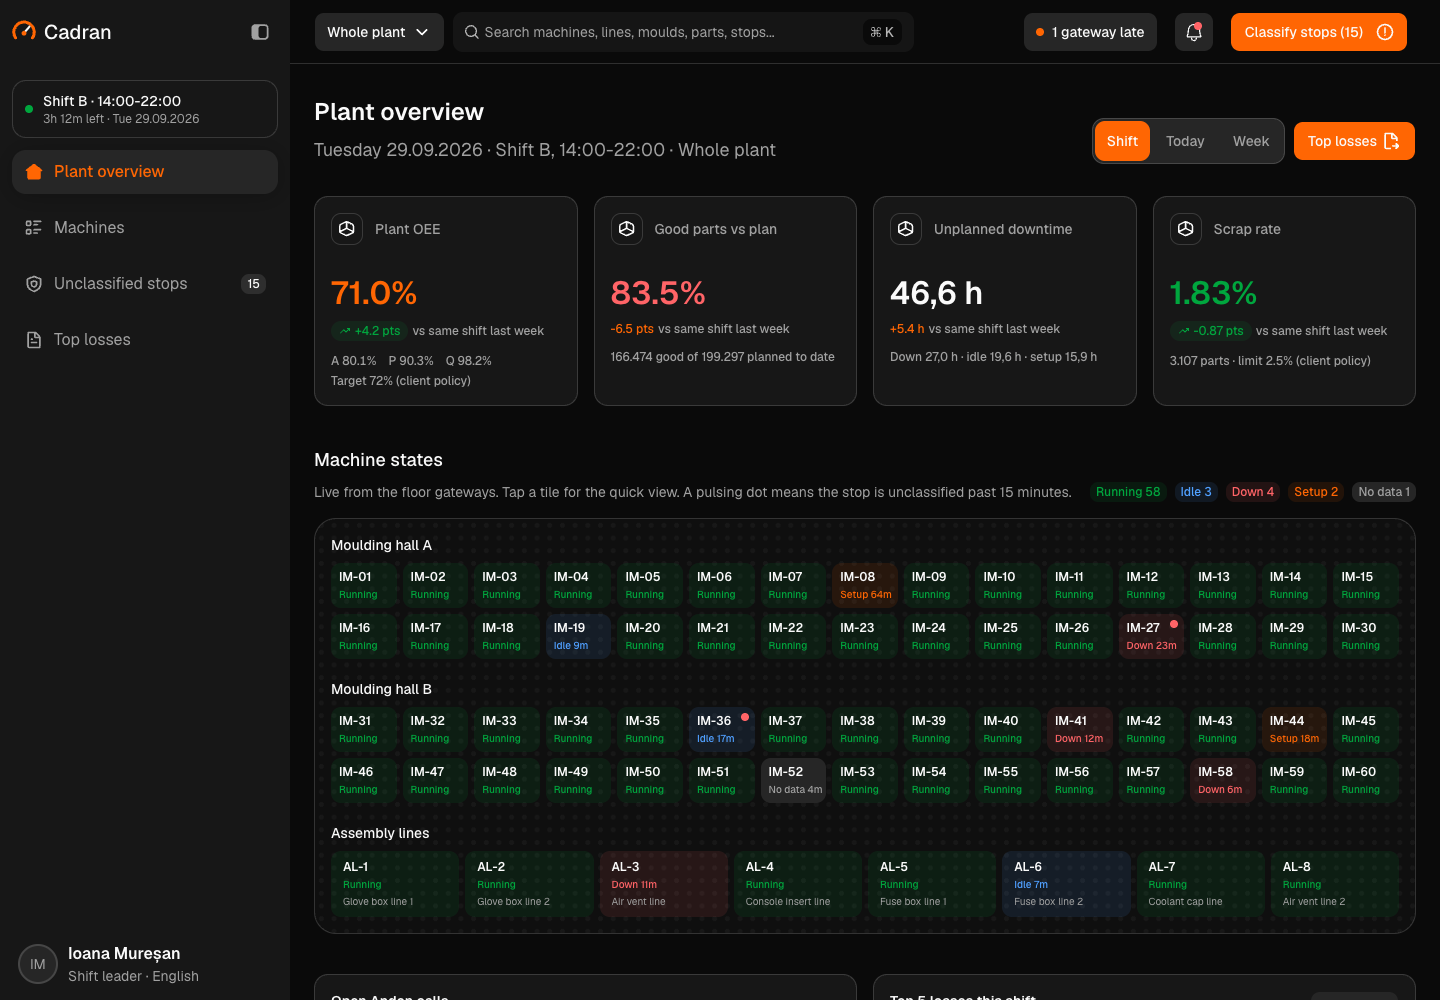
Cadran - Machine Telemetry and OEE Platform for an Injection Moulding Plant
Designed and built a clickable machine telemetry and OEE platform for a Romanian injection moulding and assembly plant that supplies automotive Tier 1 customers: live state of 60 moulding machines and 8 assembly lines, OEE with availability, performance and quality per machine, line and shift, a queue for clearing unclassified stops and a Pareto of top losses.
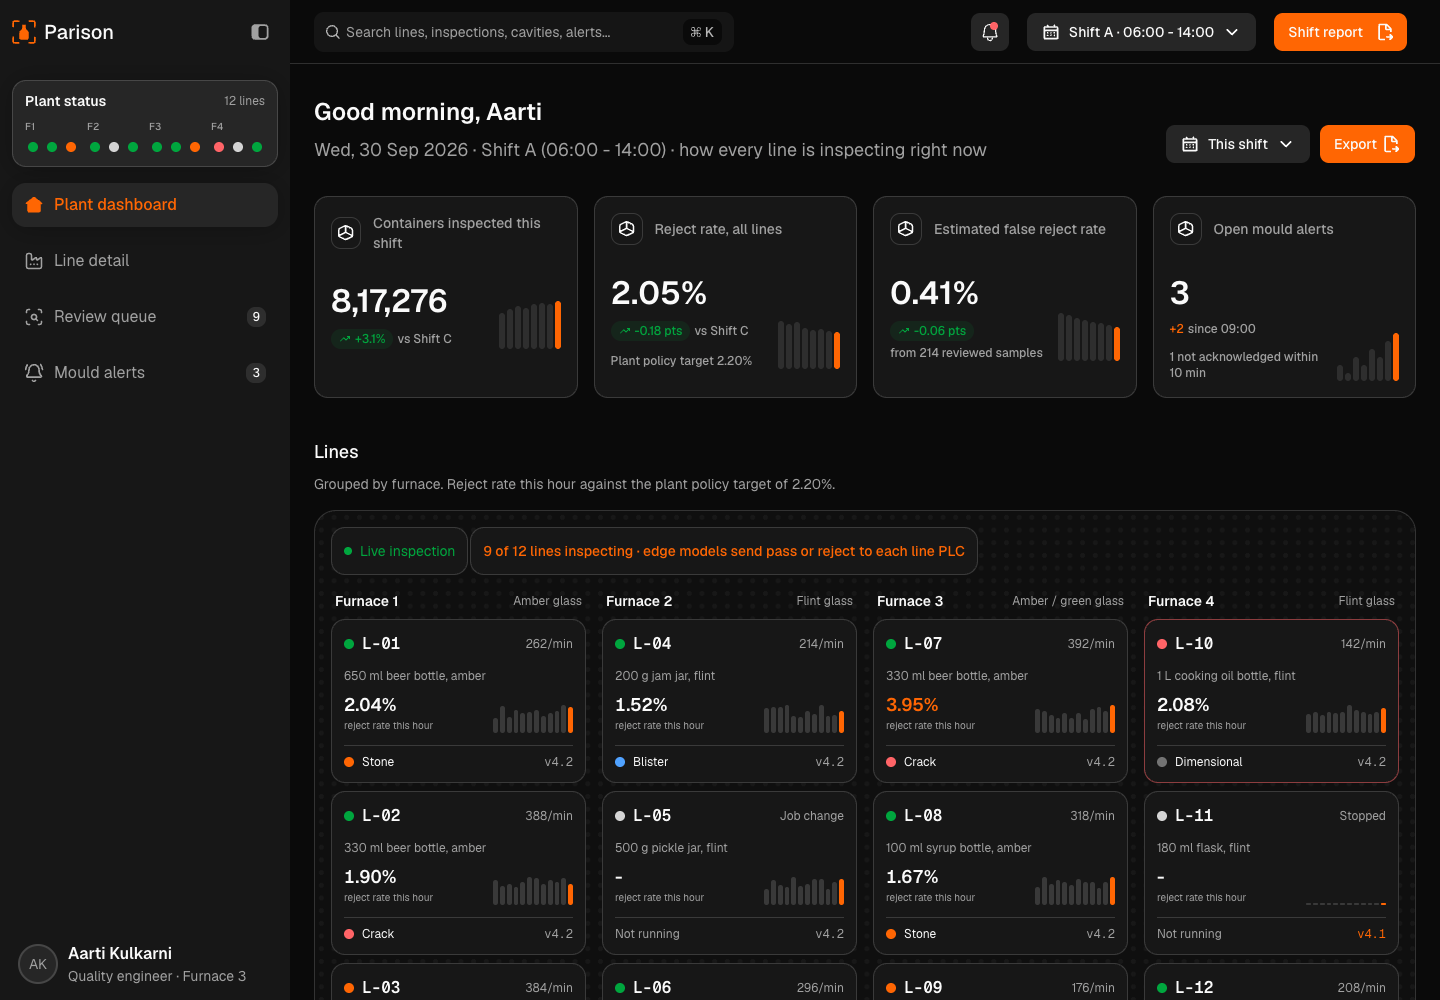
Parison - AI Visual Inspection for Glass Bottle and Jar Lines
Designed and built a clickable quality console for a glass container maker near Pune with 4 furnaces and 12 forming lines: cameras and edge models classify every bottle and jar at the cold end, uncertain images go to a person, rejects are traced to the mould cavity that made them, and every decision shows the rule behind it.
Enterprise Software Engineering - Human + AI
Contact Us
© 2026 - Copyright. All Rights reserved Oceanlab
Location
Global Headquarters
21 Merchant Road, 3rd Floor, Singapore 058267
Main corporate office and leadership operations
North America Office
548 Market Street, PMB 12345, San Francisco, CA 94104
Client operations and business development
India Office
402 Shivalik Shilp II, SG Highway, Ahmedabad 380015
Engineering and delivery center

Enterprise Software Engineering - Human + AI
Contact Us
Locations
Global Headquarters
21 Merchant Road, 3rd Floor, Singapore 058267
Main corporate office and leadership operations
North America Office
548 Market Street, PMB 12345, San Francisco, CA 94104
Client operations and business development
India Office
402 Shivalik Shilp II, SG Highway, Ahmedabad 380015
Engineering and delivery center
© 2026 - Copyright. All Rights reserved Oceanlab